



A customer audit accepts product compliance as proven only when the evidence links a specific product to a specific set of requirements, a controlled production route, and verifiable results. A certificate on its own rarely closes that chain. Auditors usually test whether the document applies to the exact item supplied, whether it is current, and whether records show that the approved condition was maintained through manufacture, finishing, packing, and release.
For a cabinet hinge, this may involve the base-metal grade, plating specification, cycle-test record, restricted-substance declaration, and lot traceability. For an electric motor, the evidence may connect the rated voltage, insulation system, protection class, winding test, and final inspection record. A packaging film file may need resin identification, thickness tolerance, migration or food-contact evidence where required, and batch-level quality data. The documents differ, but the audit logic remains the same: requirement, applicability, objective evidence, and traceability must align.
Start with the requirement that actually governs the product
Compliance cannot be demonstrated against an undefined target. The first document an auditor may seek is the controlled product specification, purchase requirement, drawing, approved sample record, contract appendix, or technical agreement that establishes what the product must meet.
This source should identify the relevant product version and the conditions of use. A statement that a screw is corrosion resistant, for example, is incomplete without the applicable finish, coating thickness or process class where specified, base material, test method, exposure condition, and acceptance criteria. A zinc-coated fastener intended for indoor furniture hardware cannot automatically support the same claim for humid storage, coastal shipment, or outdoor installation.
Requirements can arise from several places at once:
- Customer-controlled requirements: drawings, approved color panels, packaging instructions, performance limits, labeling rules, and supplier manuals.
- Product-specific legal or regulatory obligations: material restrictions, chemical disclosure, electrical safety, consumer-contact limitations, or marking obligations that apply in the intended destination and application.
- Declared voluntary standards: a standard only becomes audit-relevant when it is contractually required, legally applicable, referenced on product literature, or otherwise claimed for the supplied item.
- Internal controls that support an external requirement: work instructions, inspection plans, validated process windows, and release criteria.
A common weakness is relying on a broad statement such as “compliant with customer requirements” without retaining the revision of those requirements. When a drawing revision changes a hole pattern, load limit, finish code, adhesive cure condition, or packaging label, older records may remain valid for earlier production but cannot prove the current configuration. Revision status is therefore part of compliance evidence, not merely document administration.
Certificates are supporting evidence, not the entire proof
Certificates have different purposes and should be judged accordingly. A system certificate can show that a management system has been assessed within a stated scope. A material certificate can report the properties of a supplied raw material or component lot. A test certificate can report results from a laboratory or controlled test activity. A declaration can state that a product meets identified requirements. None of these documents automatically proves that every shipped unit conforms.
Auditors often examine the connection between the certificate and the audited product. Useful questions include: Does the part number match? Does the material grade match the bill of materials? Is the issuing organization identifiable? Does the test report identify the method and specimen? Is the date relevant to the production lot? Does the declared scope cover the destination, intended use, and product construction?
Consider an adhesive used in assembled furniture. A safety data sheet describes hazards and handling information; it does not prove bond performance in the finished assembly. A technical data sheet may state cure conditions and typical performance; it does not prove that the production batch was mixed, applied, cured, and stored within those conditions. Product compliance may therefore require the adhesive batch record, storage log, ratio or viscosity control where applicable, cure verification, and an assembly test linked to the finished product.
Similarly, a declaration concerning restricted substances should identify the product or homogeneous materials covered, the basis of the declaration, the date, and the responsible issuing entity. A generic declaration for “metal hardware” may be too broad where a hinge includes steel, brass, plastic caps, lubricant, paint, and a plated surface. The declaration needs enough product definition to show that substitutions have not moved the supplied item outside the assessed scope.
Traceability turns documents into audit evidence
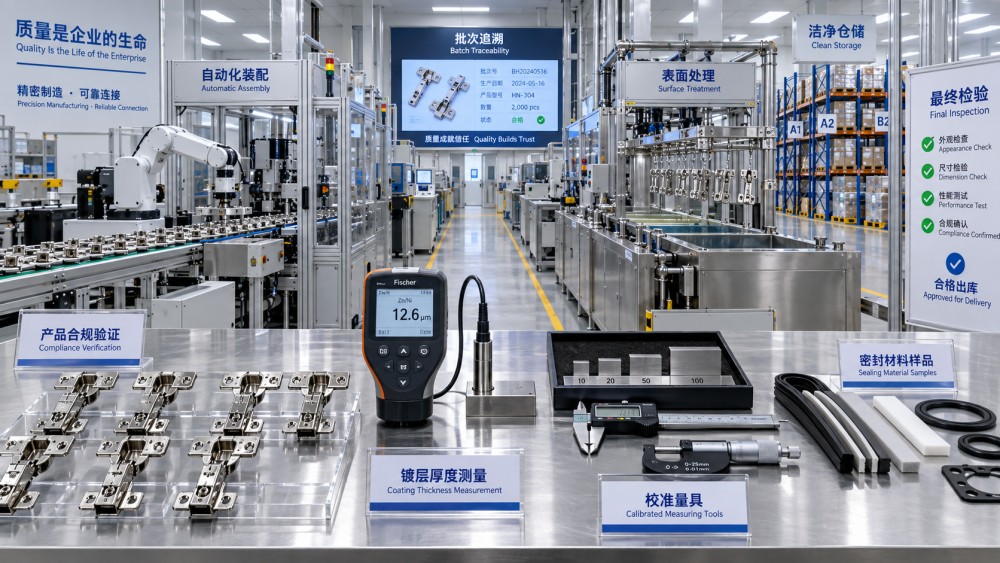
Traceability is the ability to follow the product backward from a shipment or finished lot to the records that substantiate it. The level of traceability should match the consequence of failure, contractual terms, product complexity, and how easily product lots can be mixed. It does not always require individual serial numbers. Lot, date, line, shift, purchase batch, or work-order identifiers may be sufficient when they create an unbroken and usable link.
An audit trail for a plated drawer slide could begin with a shipping label and carton code. That code should lead to the finished-goods lot, final inspection result, assembly record, incoming material records for critical components, surface-treatment batch, thickness or appearance inspection, and the applicable specification revision. If the coating was outsourced, the chain should also connect to the outsourced-process record and the received verification record.
The strength of the trail is tested when a record is sampled rather than selected in advance. If a batch number on a certificate does not appear on incoming labels, if a test report references a different product family, or if finished cartons can contain mixed lots without control, the evidence becomes difficult to defend. Digital systems are useful only when the data fields are controlled and records reflect physical identification on the floor and in the warehouse.
Lot identity must survive ordinary handling
Traceability often fails during repacking, bulk storage, rework, or transfer between processes. Loose fasteners may be poured into common bins; printed cartons may be separated from their labels; ceramic articles may be sorted after firing; film rolls may be slit and relabeled. Each transfer point needs a practical rule for preserving identity. A handwritten label without a controlled reference, for example, can create ambiguity if multiple shifts use the same product code.
Rework deserves particular attention. Reworked items may be compliant, but records should show the reason for rework, the disposition decision, the operations repeated, the inspection repeated after rework, and how the item was returned to normal stock. Rework that changes a safety-relevant or customer-visible characteristic, such as electrical insulation, coating appearance, printed artwork, adhesive cure, or load-bearing geometry, cannot be treated as a routine stock adjustment.
Testing must represent the item and its claimed condition
A test result is meaningful when the sample is representative, the method is suitable, and the acceptance criterion is known. A laboratory report with an impressive result can still be weak audit evidence if it tested a predecessor model, an unrepresentative material grade, or a product before a later design change.
Sample selection matters especially where performance is affected by variation in process conditions. Coating adhesion depends on substrate preparation, pretreatment, film build, cure profile, and handling. A thickness reading alone does not establish adhesion or corrosion resistance. In printed packaging, ink adhesion and rub resistance may change with substrate surface energy, curing, coating, and storage conditions. For a motor, a no-load functional result does not necessarily demonstrate performance under the intended load, temperature, or voltage range.
Test methods should be visible enough for an auditor to understand what was measured. This does not require disclosing confidential formulas or proprietary settings. It does require clarity on specimen identity, relevant condition, method reference or controlled procedure, measured result, acceptance criterion, date, and approval. Where external testing is used, the product description and submitted sample details should be checked against the current production configuration before the report is relied upon.
Controlled processes are evidence when inspection cannot reveal every defect
Some compliance characteristics cannot be fully verified after production without destroying the item, consuming excessive time, or missing hidden defects. In these cases, evidence from the process itself carries substantial weight.
Heat treatment of fasteners, adhesive bonding, plating, powder coating, welding, sterilized or clean packaging applications, and electrical winding are examples where process parameters influence final conformity. A final visual inspection cannot confirm that an adhesive reached its intended cure. A finished bolt may meet a simple dimensional check while having an incorrect hardness profile. A bright plated component may still have inadequate surface preparation beneath the coating.
Relevant process evidence can include approved work instructions, machine settings or recorded operating ranges, batch identification, first-piece verification, operator qualification where required by the process, environmental controls, preventive maintenance records, and response records for excursions. The purpose is not to create paperwork around every operation. It is to show that variables known to affect a required characteristic were controlled and that departures were evaluated before release.
Calibration records belong in this chain when measurements support acceptance. A thickness gauge, torque device, insulation tester, weighing scale, or color instrument is only useful evidence when its status was valid at use, its capability fits the required tolerance, and the recorded value can be interpreted. A measurement result without units, test location, or defined acceptance range is often less useful than expected.
Change control determines whether older proof remains valid
Compliance evidence has a limited life whenever the product or its production route changes. Material substitutions, alternative plating sources, revised pigment systems, new mold cavities, modified curing equipment, relocated assembly lines, firmware changes, altered packaging, and changed subcomponents can all affect the applicability of prior proof.
Not every change requires full retesting. The required response depends on the characteristic affected and the rationale supported by technical review. Replacing a carton supplier may primarily require confirmation of print, dimensions, and transport performance. Replacing a polymer grade in an electrical housing may affect flammability, mechanical strength, chemical resistance, and prior safety evidence. A different lubricant on a sliding fitting may alter opening force, contamination risk, odor, or compatibility with adjacent plastics.
A credible change-control record identifies the proposed change, affected part numbers or configurations, risk review, evidence required before release, customer approval where contractually required, implementation date, and segregation of old and new stock. It should also prevent a familiar error: using a historical test report to support a revised product because the commercial name did not change.
Nonconformities do not erase compliance when they are controlled
Auditors do not expect a record set with no defects, rejects, or deviations. They look for evidence that nonconforming material was identified, contained, evaluated, and prevented from unauthorized shipment. Missing records are often more damaging than the original defect because they leave release status uncertain.
A useful nonconformance record distinguishes between a product that failed a requirement, a measurement result under review, and a document discrepancy. It identifies the affected lot, quantity or location, immediate containment, technical disposition, required reinspection, and authorization. When a concession is used, the approval must cover the actual deviation, product lot, destination, and validity period. A verbal approval or an email that does not identify the deviation precisely is difficult to audit and easy to misapply.
Customer audits are most efficient when records can answer a sample-based question quickly: What was shipped, what requirement applied, what evidence supports it, and what happened if the normal process was interrupted? When those links are maintained in ordinary operations, proof of product compliance becomes a defensible product history rather than a folder assembled shortly before the audit.
Related News
- 00
0000-00
How to choose workspace organization racks for high-traffic areas - 00
0000-00
What Counts as Proof of Product Compliance During Customer Audits? - 00
0000-00
How to assess metal material compatibility before joining dissimilar metals - 00
0000-00
How to vet material application suppliers before requesting quotes - 00
0000-00
How supply chain disruptions affect inventory costs for importers
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.