



Buyers verify industrial hardware quality by comparing the product against a defined application requirement, then checking whether the supplier can repeatedly meet that requirement through material control, dimensional inspection, functional testing, traceable documentation, and consistent production processes. Product photos, a familiar material name, and a low defect claim may help screen suppliers, but none proves that a hinge, bolt, bearing, pump component, or anchor will perform reliably after installation.
The level of verification should reflect the consequence of failure. A cosmetic cabinet pull and a fastener used in load-bearing equipment do not deserve the same approval process. Yet the underlying discipline is similar: define what the part must do, identify the measurable characteristics that support that function, inspect representative samples, and verify that the production system can preserve the same result after the first order.
Start with the operating condition, not the catalog specification
“Stainless steel,” “heavy duty,” “high precision,” and “corrosion resistant” are not sufficient quality requirements. Each can describe products with very different performance levels. Buyers need to convert the intended use into a short set of acceptance criteria before comparing quotations.
For furniture hardware, the relevant questions may include door weight, opening frequency, mounting substrate, humid or dry use, adjustment range, and visible finish requirements. A cabinet hinge may appear substantial in a sample but develop play after repeated cycles if the pivot, spring, rivet, or mounting plate is poorly controlled. Drawer slides should be judged by their load rating under the intended installation geometry, extension type, smoothness, locking function where required, and behavior when the load is not evenly distributed.
For fasteners, the application determines whether thread accuracy, tensile properties, hardness, coating thickness, locking performance, or corrosion resistance carries the greatest weight. A screw that drives easily into a soft substrate may be unsuitable for a joint exposed to vibration. A plated bolt may look clean on arrival while its coating system provides inadequate protection in a damp, salt-exposed, or chemically active environment.
Electromechanical components require the same discipline. With bearings, buyers may need to define load direction, rotational speed, contamination exposure, noise limits, lubrication conditions, fit tolerance, and expected service interval. With pumps or motors, operating medium, temperature, duty cycle, pressure or flow requirements, electrical conditions, mounting arrangement, and sealing compatibility all shape the quality assessment.
A useful purchase specification separates three categories:
- Critical functional requirements: load, torque, strength, flow, speed, holding force, bond performance, or other performance measures tied to failure risk.
- Interface requirements: dimensions, thread form, hole pattern, mounting position, electrical connection, fit, and assembly tolerance.
- Appearance and handling requirements: finish consistency, burr control, edge condition, color, packaging, labeling, and ease of installation.
This prevents a common sourcing error: approving a part because it satisfies visible requirements while overlooking the characteristics that determine field performance.
Verify the material claim at the level that matters
Material is often treated as a simple checkbox, but material names are broad categories. Steel, stainless steel, zinc alloy, aluminum alloy, brass, nylon, and rubber can each cover multiple grades and formulations with different strength, machinability, corrosion behavior, dimensional stability, and cost.
Buyers do not always need laboratory-level analysis for every purchase. They do need a material requirement that is proportional to the application. If a decorative fitting is used indoors and carries little load, the material grade may be less important than surface quality and structural integrity. If the same component will be installed near moisture, cleaning agents, heat, or mechanical stress, the material and coating choice should be more tightly defined.
For metal hardware, ask the supplier to identify the base material, rather than accepting a generic category. Confirm whether a component is solid material, stamped sheet, die-cast alloy, powder-metal part, or a plated construction. These manufacturing routes can all be appropriate, but they behave differently. A die-cast handle with a well-applied coating can be suitable for many uses; it should not be treated as interchangeable with a solid forged or machined part in a high-load application.
For adhesives and sealants, quality verification must extend beyond a general label such as “industrial grade.” Bond strength depends on substrate preparation, joint design, cure conditions, temperature, humidity, chemical exposure, and shelf life. The relevant question is whether the adhesive performs on the buyer’s actual substrates and production process. A strong result on one material does not automatically transfer to coated metal, low-energy plastic, ceramic, paperboard, or porous wood.
Where material performance is safety-critical, regulated, contractually specified, or likely to create significant warranty exposure, buyers should request supporting documents tied to the supplied batch or production lot where feasible. Documentation is useful only when it identifies the product clearly and can be linked to the goods received. A generic certificate with no part number, lot number, issue date, or responsible issuer offers limited assurance.
Dimensional accuracy is more than passing a caliper check
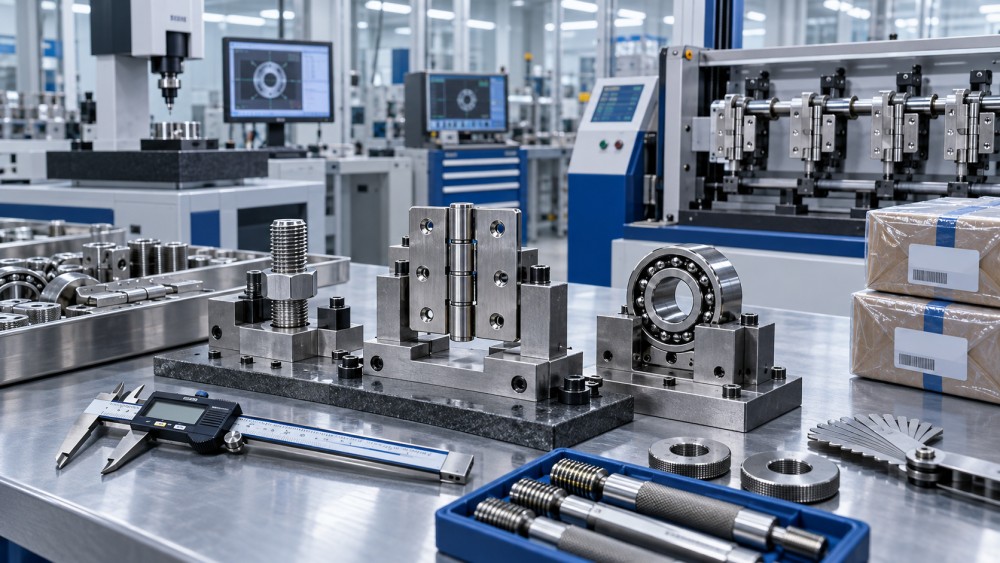
Industrial hardware frequently fails during assembly rather than during a basic incoming inspection. A part can meet one or two headline dimensions and still cause misalignment, stripped threads, poor fit, inconsistent motion, or excessive installation time.
Buyers should identify the dimensions that control interchangeability. For a hinge, that may include cup diameter, cup depth, screw-hole spacing, overlay geometry, arm position, and mounting-plate interface. For a threaded fastener, diameter alone is insufficient; thread pitch, effective thread length, head geometry, recess depth, shank length, and coating buildup can affect installation. For a bearing, bore, outside diameter, width, runout, and fit-related tolerances may matter more than a nominal size printed in a listing.
Inspecting a few samples with hand tools is a sensible first screen, but it cannot establish production consistency. For recurring purchases, buyers should ask how dimensions are controlled during manufacturing and which characteristics are checked on each batch. A supplier that can identify critical dimensions, state the inspection method, and provide clear tolerance limits is easier to manage than one that merely states “standard size” or “high accuracy.”
Functional gauges, assembly fixtures, thread gauges, go/no-go inspection, and controlled measuring equipment are often more revealing than a random collection of measurements. The objective is not to demand an elaborate quality system for every commodity part. It is to ensure that inspection reflects the way the part will be used.
Compare finish quality by performance, not appearance alone
Surface finishing has a dual role. It may define the product’s visible character, especially for furniture and office hardware, while also protecting the base material from corrosion, wear, fingerprints, cleaning chemicals, or handling damage. A uniform-looking finish is therefore only the first part of the assessment.
Buyers should examine samples under normal viewing conditions and under practical handling. Look for color variation, thin coverage at edges, pinholes, blistering, sharp burrs, scratches, inconsistent brushing, poor polishing, and residue around moving or threaded areas. On plated, painted, powder-coated, or anodized parts, inspect corners, holes, recesses, weld areas, and interfaces where coverage is more difficult to maintain.
The finish requirement should match the environment. Indoor decorative hardware may prioritize color consistency and resistance to routine cleaning. Hardware exposed to humidity, outdoor conditions, industrial dust, frequent abrasion, or chemicals requires a more demanding evaluation. Buyers should avoid assuming that a thicker-looking coating is automatically better. Adhesion, substrate preparation, coating chemistry, curing, edge coverage, and handling during packing all influence durability.
For visible product ranges, approve a physical finish standard rather than relying only on digital photos or descriptive terms such as matte black, brushed nickel, antique bronze, or champagne gold. Lighting, camera processing, and display settings can obscure meaningful variation. A retained approved sample, identified by part number and revision, creates a more reliable reference for future shipments.
Test the failure mode that matters in use
Quality control becomes credible when the supplier can demonstrate performance connected to the part’s likely failure mode. The right test differs by product category, and buyers should be cautious of test claims that are impressive but unrelated to the intended application.
For motion hardware, useful checks can include cycle performance, opening or closing consistency, load behavior, lateral stability, damping performance, and retention of adjustment after use. For fasteners, pull-out, torque, proof load, thread engagement, vibration resistance, or corrosion exposure may be relevant depending on the assembly. For bearings, noise, rotational smoothness, clearance, temperature behavior, and contamination tolerance may be more useful than a broad claim of long service life.
For pumps, valves, and related equipment, the test should reflect the operating medium and duty conditions as closely as practical. A water-based bench test cannot fully establish suitability for viscous fluids, particles, elevated temperatures, or chemically aggressive media. It may still be valuable, but the buyer should understand its limits.
For adhesives, use a test coupon and curing process that resemble the final joint. A bond tested after a convenient curing period in a controlled room may not predict performance when the buyer’s line applies a different bead thickness, experiences temperature variation, or loads the joint before full cure. Where the application is important, production trials should assess both immediate process behavior and the cured joint’s expected service conditions.
Functional verification also needs a realistic sample plan. One perfect pre-production sample does not prove that a production order will match it. Buyers should distinguish among:
- Reference samples: used to confirm design, finish, fit, and intended function before ordering.
- Pre-production samples: used to verify that the chosen factory process can reproduce the approved design.
- Production inspection samples: drawn from the completed order or defined lots to check ongoing conformity.
That distinction is particularly important when a supplier has made tooling changes, changed a plating subcontractor, substituted raw material sources, or moved production between facilities.
Assess the supplier’s ability to control variation
A buyer is not only approving an item; they are approving a process that must continue producing that item. The most expensive quality problems often appear after the first shipment, when an initially acceptable sample is followed by material variation, uneven finishing, inconsistent assembly, missing components, or packaging damage.
Questions about quality control should be specific enough to reveal how the supplier works. Which incoming materials are checked? Which dimensions are considered critical? At what production stage is the finish inspected? How are nonconforming parts separated? Can the factory trace a complaint back to a production date or lot? Who approves substitutions in material, tooling, process, or subcontracted operations?
A supplier does not need to use the buyer’s terminology to have effective controls. However, vague answers should affect the buyer’s risk assessment. Statements such as “our workers inspect everything” provide less confidence than a simple, documented explanation of checkpoints, acceptance limits, and corrective action.
Packaging deserves attention here. A sound component can arrive unusable if loose metal parts rub together, plated surfaces contact abrasive material, moisture enters cartons, or quantities are mixed. For components used in line assembly, labeling, count accuracy, lot marking, and pack configuration can be as operationally important as the part itself.
Use documents as evidence, not as a substitute for inspection
Drawings, declarations, inspection reports, test records, material certificates, and compliance statements can reduce uncertainty, especially when the buyer has clear internal or customer requirements. They should support a verification process rather than replace it.
Before relying on any document, check four points: does it identify the exact product configuration; does it relate to the relevant batch, material, or process; does it address the property that matters for the application; and does the issuer have a clear connection to the manufacturing or test activity? A report for a similar component, an older revision, or an unspecified sample may have little value.
Compliance requirements should also be defined early. Hardware may be subject to material restrictions, product-specific safety rules, customer specifications, or destination-market obligations depending on its final use. Buyers should communicate the intended market and application rather than assume that an exporter’s general statement applies to every configuration.
Build approval around the cost of a wrong decision
There is no single inspection checklist that suits every industrial hardware purchase. Excessive verification adds cost and time to low-risk consumables; minimal verification can be costly for components that affect safety, assembly throughput, customer-facing appearance, or warranty exposure.
A practical approach is to increase scrutiny when a part is difficult to replace after installation, carries a load, affects a moving mechanism, faces corrosive conditions, interfaces with tightly controlled assemblies, or is supplied under a customer specification. In those cases, a controlled drawing, approved reference sample, documented inspection criteria, and shipment-level checks are usually justified.
For simpler, low-consequence hardware, a clear specification, dimensional confirmation, finish review, and periodic incoming checks may be enough. The important discipline is consistency: quality should be defined by the hardware’s job in the finished product, then verified through evidence that is relevant to that job. Price comparisons become more meaningful once buyers know whether they are comparing truly equivalent parts.
Related News
- 00
0000-00
How does order volume affect the price of self-adhesive label materials? - 00
0000-00
How backlash affects precision mechanical transmission accuracy - 00
0000-00
How Do You Choose Drawer Slides for Heavy Storage? - 00
0000-00
Choosing a Gearbox for Automation Systems: Torque, Backlash, and Duty Cycle - 00
0000-00
What to verify before choosing a furniture connectors supplier
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.